

Hose Clamps vs. Snap-Fit Technology: The Ultimate Guide to Dust Leak Prevention in Factories
Direct-Answer Block
Q: Why do flexible connectors leak powder at the clamp edge?
A: A hose clamp creates a concentrated compression zone where the flexible sleeve is restrained against the pipe. Under vibration, the boundary between the clamped area and the freely flexing wall becomes a fatigue initiation point — the sleeve tears along that line, and powder escapes. Snap-fit technology removes the failure mechanism entirely: the sleeve engages a spigot groove through a spring-steel band in an exterior pocket, so the flexing wall is never compressed at a single edge.
The Real Source of Dust Leaks: It Is Rarely the Sleeve
When a powder-processing line leaks, maintenance teams often replace the sleeve — only to see the leak return. The sleeve wall is rarely the root cause. The failure is at the interface: the point where the connector meets the pipe.
Two interface designs dominate, and they fail very differently:
| INTERFACE | HOW IT SEALS | FAILURE MODE |
|---|---|---|
| Hose Clamp (HC) | External clamp compresses sleeve against pipe OD | Pinch-point tear → dust leak |
| Snap-Fit (SF) | Spring-steel band in exterior pocket locks sleeve into spigot groove | No compression of flexing wall → no tear point |
The difference is not the material. It is whether the interface compresses the wall that must flex.
The Physics of the Pinch Point
A hose clamp works by squeezing the sleeve radially against the pipe. This creates a rigid ring at the clamp location.
The sleeve has to flex during operation — to absorb vibration, offset, and pressure pulses. The area directly under the clamp cannot flex; the area just outside the clamp flexes freely.
That boundary is a stress concentration point. Under repeated 20–30 Hz vibration, the material at the boundary fatigues first. The failure is progressive: micro-cracks initiate, propagate, and eventually open into a tear — releasing powder.
The Three-Step Failure Sequence
- Compression — the clamp squeezes the sleeve into a rigid ring.
- Flex boundary — vibration concentrates stress at the edge of the clamp.
- Fatigue tear — the wall cracks along the clamp line, and powder escapes.
This is why clamp-edge tears are the most common dust leak in powder conveying.
How Snap-Fit Technology Eliminates the Pinch Point
Snap-fit technology changes where the retention force is applied.
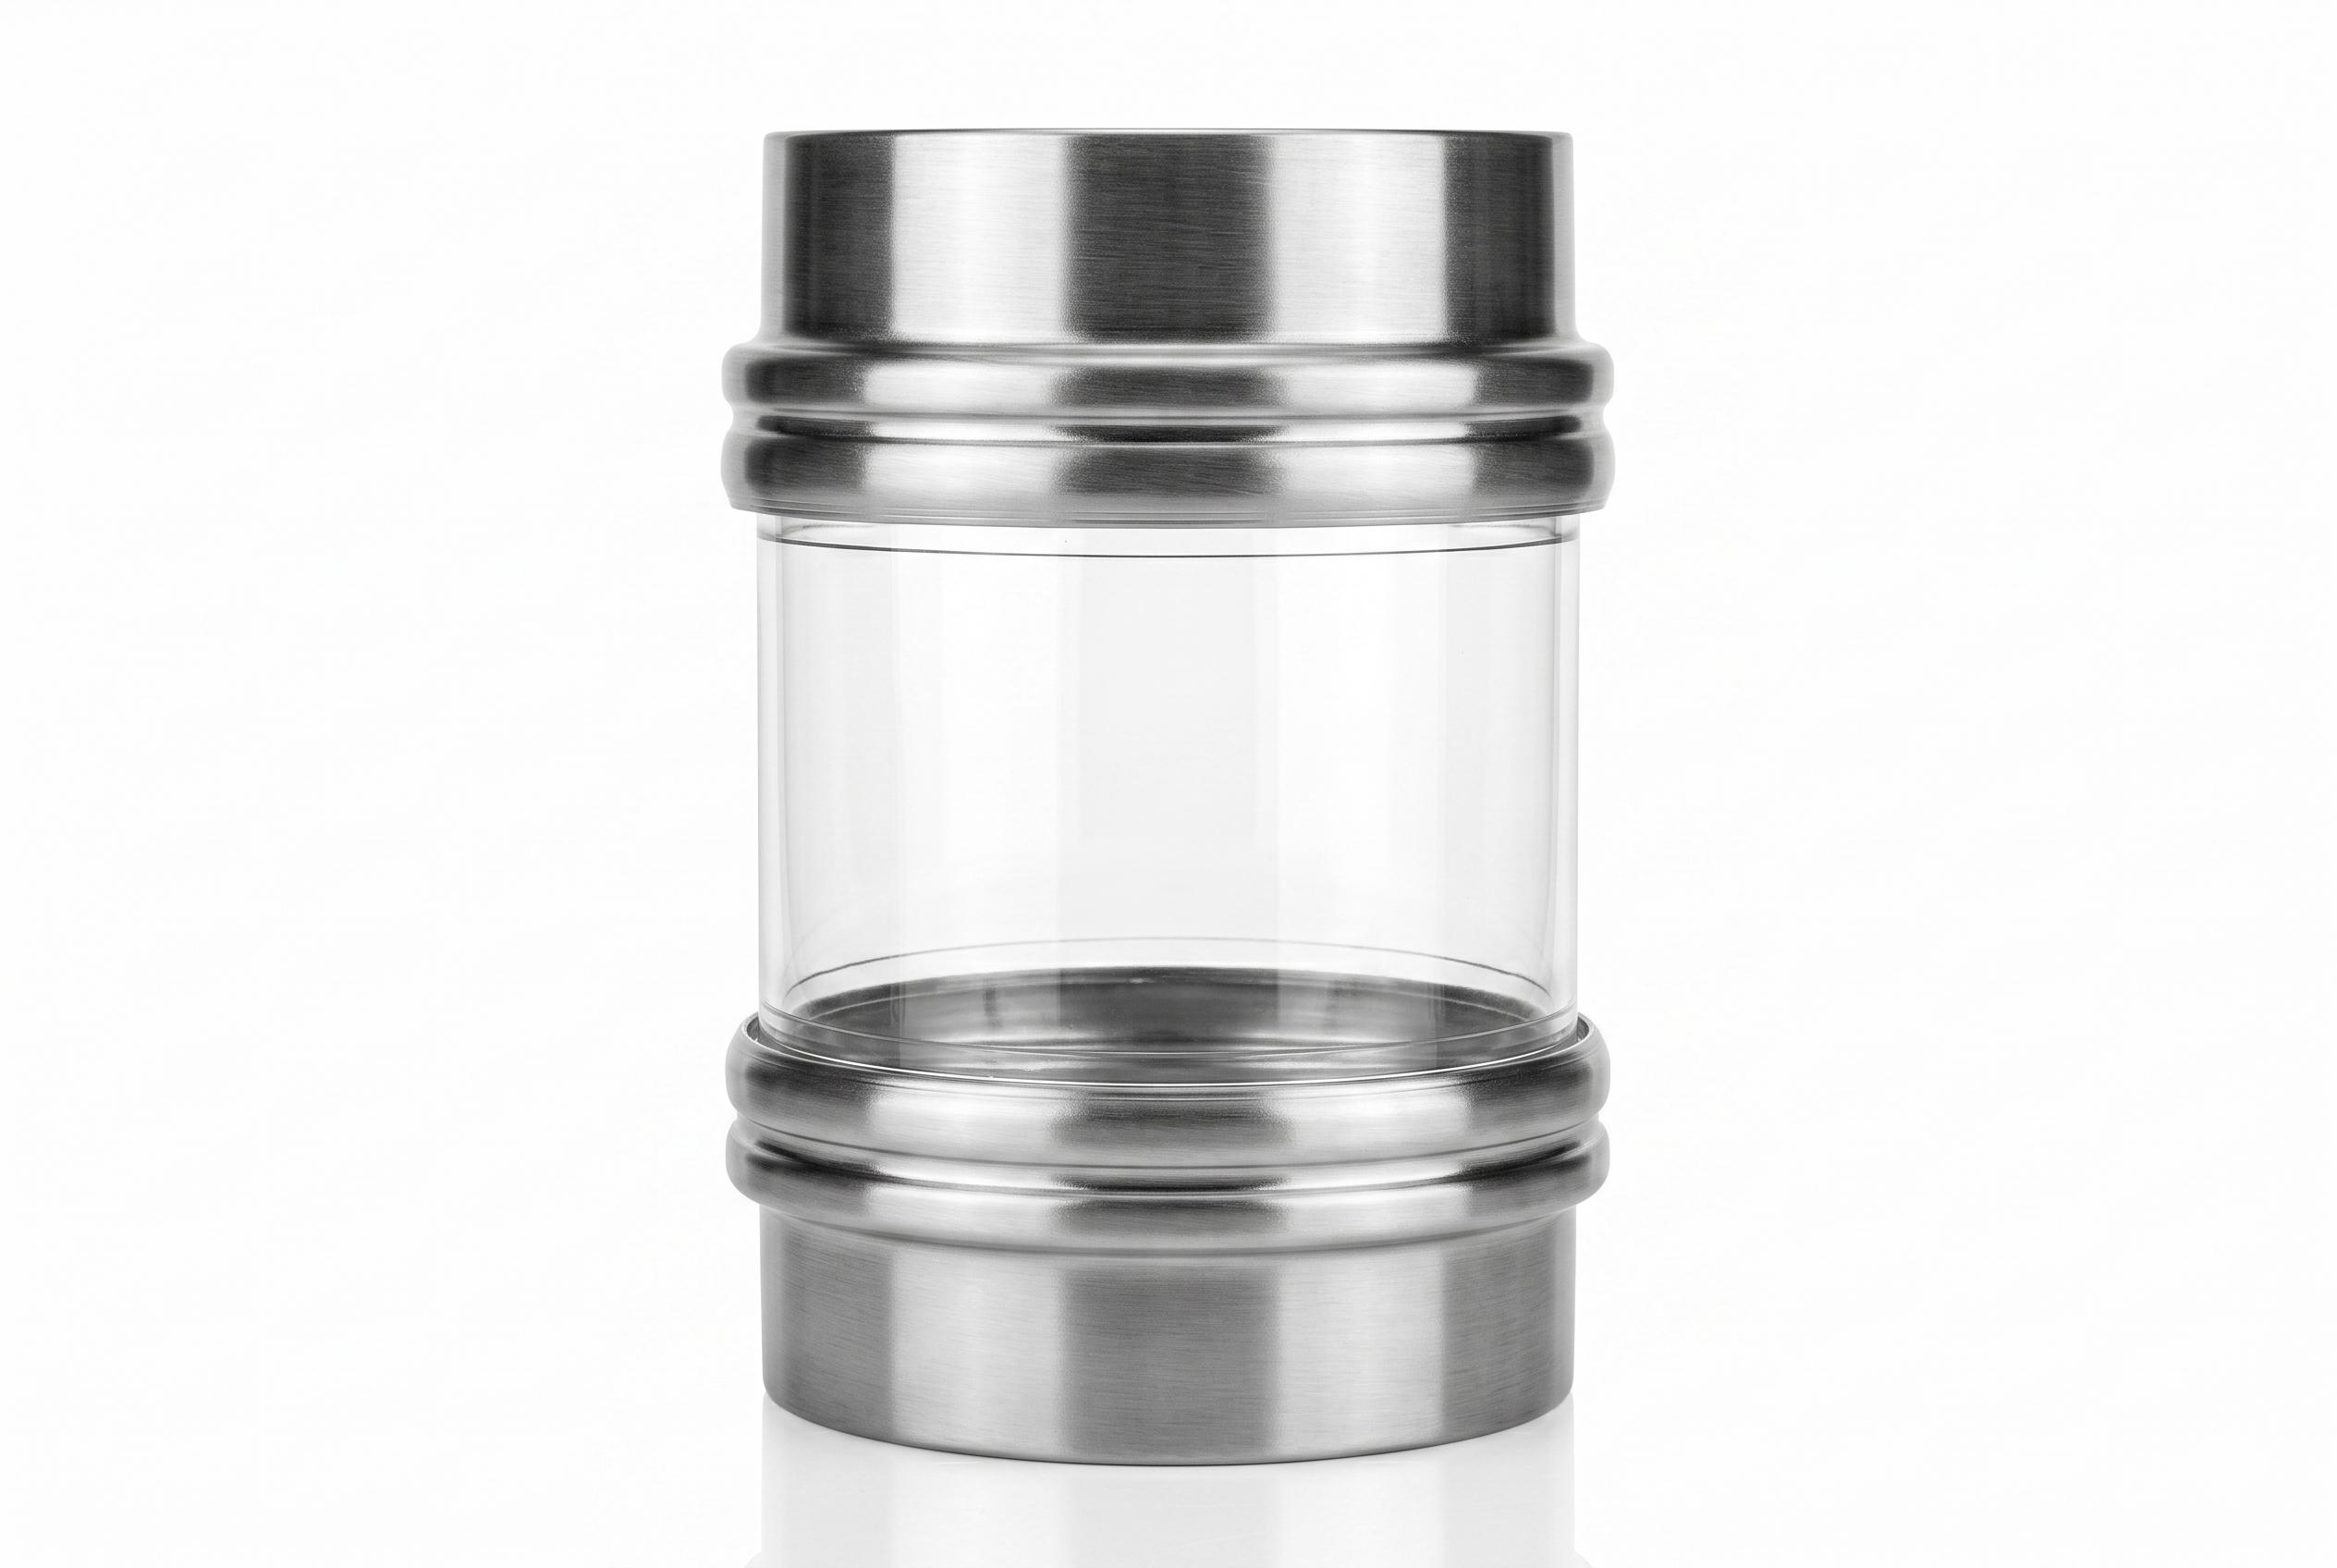
Instead of compressing the flexing wall, a snap-fit connector seats a spring-steel band inside an HF-welded exterior pocket. The band engages an internal groove on a welded spigot. The retention is mechanical engagement, not radial compression.
Result:
- The flexing wall is never squeezed at a single edge
- No stress concentration point forms
- The sleeve flexes uniformly along its full length
- Powder stays contained even under sustained vibration
Comparison Table: Hose Clamp vs Snap-Fit
| FACTOR | HOSE CLAMP (HC) | SNAP-FIT (SF) |
|---|---|---|
| Retention mechanism | Radial compression | Mechanical engagement in spigot groove |
| Flexing wall compressed | Yes — at clamp ring | No |
| Stress concentration point | One, at clamp edge | None |
| Tear initiation under vibration | High | Eliminated |
| Dust leak resistance | Poor over time | Excellent |
| Changeout tools | Clamp tool required | Tool-free |
| Metal in product bore | Clamp sits outside; sleeve wall still flexes against it | Spring-steel band in exterior pocket — bore stays flush |
Why “Metal in the Connector” Is Not the Question
A connector can contain metal without exposing metal to the product. The correct engineering question is:
“Is metal exposed to the product bore?” — not “Does the connector contain metal?”
In the SF snap-fit design, the spring-steel band is housed in an exterior pocket, never in the product path. The bore remains smooth and flush, with no crevice for powder to trap and no exposed metal hardware.
For metal-detection-sensitive processes, always evaluate the complete installed assembly — but the snap-fit architecture keeps the retention hardware out of the bore.
Locked Specifications: HC vs SF
| PROPERTY | HC HOSE CLAMP | SF SNAP-FIT |
|---|---|---|
| Wall Thickness | Varies by configuration | 1.0 mm clear polyether TPU |
| Hardness | Shore A 90 | Shore A 90 |
| Tensile Strength | 40 MPa | 40 MPa |
| Elongation | 600% | 600% |
| DIN Abrasion | 39.0 mg | 39.0 mg |
| Temp Range | −20 °C to +110 °C | −20 °C to +110 °C |
| Dust-leak risk | Pinch-point tear | No pinch point |
| Changeover | Clamp tool, 5–10 min | Tool-free, <30 sec per end |
| FDA | 21 CFR 177.2600 (TQT4821B36E) | 21 CFR 177.2600 (TQT4821B36E) |
Where Dust Leaks Cost the Most
Dust leaks are not just a housekeeping problem. They carry real operational cost:
- Product loss — escaped powder is wasted material
- Cross-contamination — leaked powder contaminates adjacent processes
- Metal-detector rejects — clamp or wire fragments trigger false rejects
- Downtime — leak repair stops the line
- Cleaning labor — spilled powder requires cleanup
- Safety — combustible dust accumulation is an explosion hazard (ATEX zones)
A leak that appears minor at the clamp edge can be the single largest recurring cost on a powder line.
How to Eliminate Dust Leaks at the Interface
- Identify the failure location. Is the tear at the clamp edge, or in the sleeve wall?
- If at the clamp edge — the interface is the problem, not the sleeve.
- Switch to snap-fit. Weld a stainless steel spigot once.
- Measure the installation gap. See the sizing guide.
- Snap the sleeve in. Tool-free, under 30 seconds per end.
- Eliminate the leak at its source — no more clamp-edge tears.
Matching Components
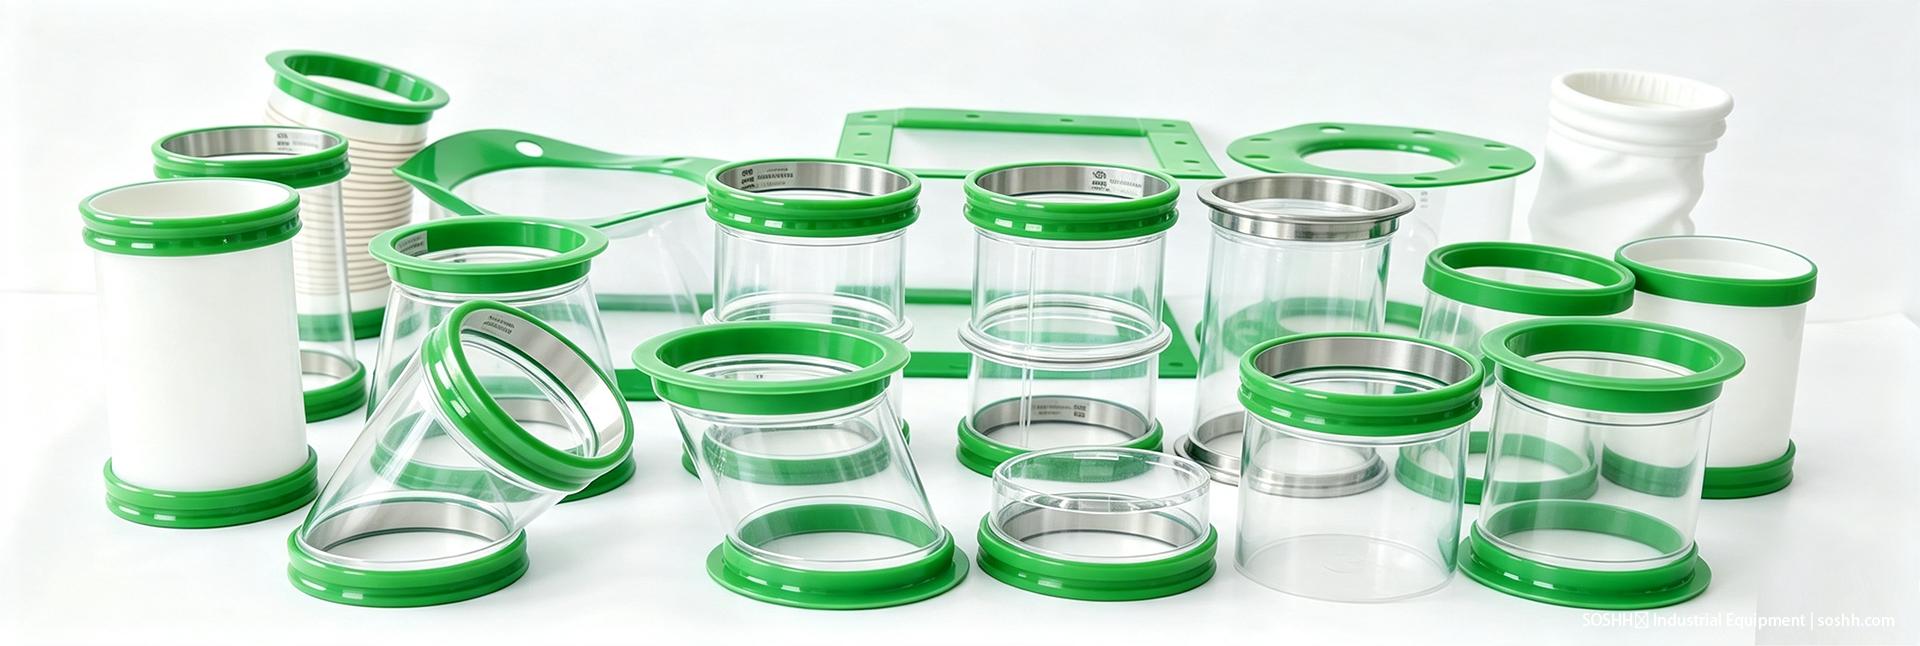
The snap-fit interface requires a rigid seating component. Pair the SF snap-fit sleeve with a sanitary stainless steel welded spigot — the spigot provides the fixed groove geometry, and the sleeve snaps in without tools.
For retrofit applications where welding is not possible, the HC hose clamp remains the no-weld path — with the clamp-edge tear trade-off described above.
Frequently Asked Questions
Q1: Why does my flexible connector keep leaking powder at the clamp edge?
A: The clamp creates a concentrated compression point. Under vibration, the sleeve fatigues and tears along the clamp line. The fix is to remove the pinch point — snap-fit technology retains the sleeve by mechanical engagement, not radial compression.
Q2: Is the sleeve material the cause of dust leaks?
A: Rarely. The sleeve wall is usually intact. The leak is at the interface — the clamp edge is the classic failure location. Replacing the sleeve without changing the interface will not stop the leak.
Q3: Does the snap-fit connector put metal in the product?
A: The retention band is a spring-steel component housed in an HF-welded exterior pocket. It is never in the product bore. The bore stays flush and smooth, with no exposed metal hardware.
Q4: Do I need tools to install a snap-fit connector?
A: No. The SF snap-fit sleeve installs tool-free in under 30 seconds per end. A line operator can complete the changeout without maintenance support.
Q5: What if I cannot weld a spigot?
A: For plain pipe ends, the HC hose clamp provides a no-weld retrofit. It is the fastest path for existing pipe, with the trade-off of the clamp-edge tear point.
Q6: Is the snap-fit sleeve food-contact compliant?
A: Yes. The sleeve is 100% virgin polyether TPU compliant with FDA 21 CFR 177.2600 (Report TQT4821B36E), 100% phthalate-free, and formulated in accordance with EU 10/2011 and EC 1935/2004.
Q7: How do I size a snap-fit connector for my line?
A: Measure spigot seating OD, static installation gap, dynamic stroke, media, temperature, and pressure/vacuum. See the How to Measure & Size guide.