1. Why Wrong Measurements Cause Connector Failures
A significant proportion of premature snap-in connector failures are traceable to measurement error rather than material defects. Four mistakes dominate:
| FAILURE MODE | ROOT CAUSE | VISIBLE SYMPTOM |
|---|
| Clamp-edge tearing | IG oversized → sleeve buckles into S-bend under vibration | Tear at the cuff pinch line, not the body center |
| Tensile fatigue | IG undersized → sleeve stretched taut at rest | Circumferential cracks mid-body |
| Snap-band disengagement | Spigot OD measured as pipe bore → cuff too loose | Sleeve slips off groove under pressure |
| Leak at one end | Two spigots measured as equal when they differ | Dust escape on the larger-diameter end |
This guide eliminates all four by specifying exactly what to measure, where, with what tool, and how to record it.
2. Measurement Toolkit
| TOOL | USED FOR | MINIMUM ACCURACY |
|---|
| Vernier caliper / digital caliper | Spigot OD (≤ 300 mm) | ±0.02 mm |
| Pi tape (Ø tape) | Spigot OD > 300 mm | ±0.5 mm |
| Steel rule / tape (rigid) | Installation gap (IG) | ±1 mm |
| Dial indicator / stroke gauge | Dynamic stroke amplitude | ±0.1 mm |
| Surface thermometer | Process + CIP temperature | ±2 °C |
| Pressure gauge | Positive / negative pressure | ±5% |
Warning: Do not use a flexible tailor tape — it stretches 3–5 mm under hand tension and corrupts the OD reading. Use a rigid Pi tape or caliper.
3. Step 1 — Measure the Spigot Outer Diameter (OD)
The spigot is the rigid metal lip or seating ring the connector cuff snaps onto. Measure the outside of the seating channel, never the pipe or duct bore.
![Snap-in flexible connector spigot OD, groove depth and cuff engagement measurement points]() Figure 1: Measure all metal connection points directly on the equipment interface. Always verify the rigid spigot OD (Outside Diameter), groove retention depth, and cuff seating profile with calipers.
Procedure:
- Power down and lock out the machine.
- Place the caliper or Pi tape around the spigot seating channel — the groove where the snap band locks.
- Measure at three circumferential positions (0°, 120°, 240°).
- Record all three values, then compute the average and the largest.
- The cuff is fabricated to clear the largest reading (not the average) to guarantee engagement.
- Repeat for both ends — upper and lower spigots are frequently different diameters.
Example recording sheet:
- Upper spigot OD: 204.1 / 204.3 / 204.5 mm → use 204.5 mm
- Lower spigot OD: 203.8 / 204.0 / 204.2 mm → use 204.2 mm
If the two spigots differ by more than ~5 mm, specify a conical/reducer sleeve — fabricated to exact millimeter dimensions.
4. Step 2 — Measure the Static Installation Gap (IG)
The installation gap is the face-to-face distance between the two spigot faces with the machine stationary and at rest. This is the single most overlooked dimension — and the most common cause of tearing.
Procedure:
- Confirm the machine is in its resting position (sifter powered off, hopper settled, no load).
- Measure the distance between the two spigot faces — not the outer flange edges.
- Take readings at four points (front, back, left, right) if the gap is uneven.
- Record the narrowest value as the static IG.
- Separately record the dynamic stroke amplitude (Step 3).
The sizing relationship:
![Static installation gap and axial vibration stroke measurement for a flexible connector showing CL greater than IG rule]() Figure 2: The sizing golden rule: The relaxed connector length (CL) must always be slightly longer than the static installation gap (IG) to accommodate vibration strokes without tensile cuff stress.
Optimal sleeve length = Static IG + Dynamic stroke amplitude + Calibrated flex radius
- IG too large → sleeve sags into an uncontrolled S-bend under oscillation → stress concentration at the clamp edge → tear.
- IG too small → sleeve permanently stretched → constant tensile stress → mid-body fatigue crack.
- Typical standard screeners: 20–35 mm static gap, 3–10 mm stroke.
Rule: Never estimate. Send both static IG and stroke amplitude in millimeters.
5. Step 3 — Measure Dynamic Stroke Amplitude
For vibrating sifters, screeners, and fluid-bed dryers, the static IG alone is insufficient. The machine’s stroke (peak-to-peak oscillation) must be added or the sleeve will tear within days.
Procedure:
- With the machine running at normal speed, use a dial indicator or stroke gauge against the moving frame.
- Record the peak-to-peak stroke amplitude in mm (typically 3–10 mm for circular screeners at 20–30 Hz).
- Note the vibration frequency (Hz) if known — it affects fatigue life.
- Send both values with the RFQ.
| EQUIPMENT | TYPICAL STROKE | TYPICAL FREQUENCY |
|---|
| Circular vibratory sifter | 3–6 mm | 20–30 Hz |
| Rectangular gyratory screener | 5–10 mm | 15–25 Hz |
| Fluid-bed dryer | 2–5 mm | 10–20 Hz |
![Four-position dynamic movement envelope for snap-in flexible connector sizing: neutral, extension, compression, lateral offset]() Figure 3: Four dynamic movement limits for vibrating equipment: Neutral (natural sag), Maximum Extension (no cuff tension), Maximum Compression (smooth outward bulge without material traps), and Maximum Lateral Offset (shearing absorption).
6. Step 4 — Special Geometry: Square-to-Round, Offset, Conical
Non-cylindrical connections require additional dimensions. Specify all that apply:
| GEOMETRY | ADDITIONAL MEASUREMENTS | EXAMPLE |
|---|
| Square-to-round | Square flange side lengths + round spigot OD | 400×400 mm square → Ø204 mm round |
| Offset (eccentric) | Centerline offset between upper and lower axes | 50 mm horizontal offset |
| Conical (reducer) | Upper OD + lower OD + vertical height | Ø254 → Ø204 over 300 mm |
| Rectangular chute | Length × width of both openings + drop height | 600×300 → 400×200 |
All non-standard geometry is CNC-cut and HF-welded from flat sheet rather than injection-molded, so custom geometry does not require dedicated mold tooling.
7. Step 5 — Specify the Tolerance (ISO 2768-m)
For a snap-in seal to work, cuff and spigot must match within controlled tolerance. Fabrication is to ISO 2768-m as standard.
| DIMENSION | STANDARD TOLERANCE | WHY IT MATTERS |
|---|
| Spigot OD (machined) | ISO 2768-m | Snap band seats into groove without over-compression |
| Sleeve cuff diameter | Matched to spigot OD | HF-welded cuff grips groove for a dust-tight seal (zero visible leakage under rated pressure) |
| Sleeve length | Calculated from IG + stroke | Prevents S-bend buckling and tensile stretch |
| Spigot surface finish | 2B (Ra < 0.8 µm) / EP (Ra < 0.4 µm) | EP specified for pharma duty |
8. Material Selection — Match to Your 4th & 5th Parameters
The sleeve material is chosen from media + temperature + pressure — not guessed:
| CODE | MATERIAL | THICKNESS | TEMP RANGE (SSOT) | TENSILE | ELONGATION | KEY USE CASE |
|---|
| PU10 | Ether TPU | 1.0 mm | −30 to +110 °C (peak +120 °C; 85 °C CIP) | 40 MPa | 600% | Standard, most common |
| PU15 | Ether TPU (heavy) | 1.5 mm | −30 to +110 °C (peak +120 °C; 85 °C CIP) | 40 MPa | 600% | Abrasive duty |
| PUAS | Anti-static TPU | 1.0 mm | −30 to +110 °C (peak +120 °C; 85 °C CIP) | 40 MPa | 600% | Combustible dust, battery |
| PUHT | High-temp PU | 1.0 mm | −20 to +150 °C | 40 MPa | 600% | Elevated temperature |
| PURF | Fiber-reinforced TPU | 0.8 mm | −30 to +110 °C (peak +120 °C; 85 °C CIP) | 300 MPa | 600% | Positive/negative pressure |
| PTFE | Virgin PTFE | 0.2 mm | −70 to +260 °C (peak +280 °C) | — | — | Corrosive, SIP steam |
| SIL | Silicone | 0.6 mm | −50 to +200 °C (121 °C SIP) | — | — | Ambient dust |
Anti-static grade (PUAS): surface resistivity 10⁶–10⁹ Ω/sq, dissipative, tested per IEC 60079-32-2. SGS-verified volume resistivity 4.02×10⁷ Ω (Report SHMR240801578301-1, per IEC 62631-3-1:2023). Suitable for assessment in ATEX Zones 20/21/22 per site hazardous-area classification; the connector is one component of the electrostatic-control system and does not replace grounding/bonding.
9. The 5-Parameter RFQ
You do not calculate the sleeve length yourself. Send these five parameters and receive a watermarked 2D outline drawing + material recommendation within 24 hours:
| # | PARAMETER | EXAMPLE | HOW TO FIND IT |
|---|
| 1 | Spigot OD (both ends) | Ø204.5 mm top / Ø204.2 mm bottom | Caliper, 3 points, use max |
| 2 | Installation Gap (IG) | 28 mm static + 5 mm stroke | Face-to-face, machine at rest |
| 3 | Media | Lactose powder / NMC / flour | Your process material |
| 4 | Temperature | 20 °C process / 80 °C CIP | Process + cleaning cycle |
| 5 | Pressure | +0.35 bar / −50 mbar | Positive or vacuum conveying |
Send to: amin@soshh.com | +86 13567045023 Subject line: RFQ — Snap-In Connector — [Company] — [ØD × L]
10. Quick Reference — Measurement Cheat Sheet
- Spigot OD (upper) ______ mm (3 points, use max)
- Spigot OD (lower) ______ mm (3 points, use max)
- Static IG ______ mm (machine at rest, narrowest point)
- Stroke amplitude ______ mm (vibratory equipment only)
- Media ______
- Temperature ______ °C (process + CIP)
- Pressure ______ bar / ______ mbar
11. Frequently Asked Questions
What is the difference between spigot OD and pipe bore? The spigot OD is the outside of the rigid metal lip the connector snaps onto; the pipe bore is the inner flow diameter. Measure the spigot OD — it is the seating surface that determines cuff fit.
Do I need to calculate the sleeve length myself? No. Send the static installation gap and stroke amplitude; engineering calculates the correct sleeve length including the calibrated flex radius.
What tolerance do you fabricate to? ISO 2768-m as standard, with spigot finish 2B (Ra < 0.8 µm) or electro-polished (Ra < 0.4 µm) for pharma duty.
Can you supply a watermarked 2D drawing before I order? Yes. A watermarked 2D outline drawing is returned within 24 hours of receiving your five parameters. 3D CAD (STEP/IGES) is provided under NDA/NNN for OEM projects.
What if my two spigots are different diameters? Specify both ODs. A conical or reducer sleeve is fabricated to exact millimeter dimensions.
Can you handle square-to-round or offset connections? Yes. Square-to-round, offset, conical and rectangular transitions are CNC-cut and HF-welded to millimeter specification.
What is your standard lead time? Standard snap-in sleeves ship in approximately 5 business days; extended lengths in 7 business days; SS304/SS316L weld spigots in 7–10 business days.
What is your minimum order quantity? 1 piece for engineering prototype testing; standard production runs start at 5 pieces per SKU. Sample fees are credited toward the first bulk PO exceeding $3,000.
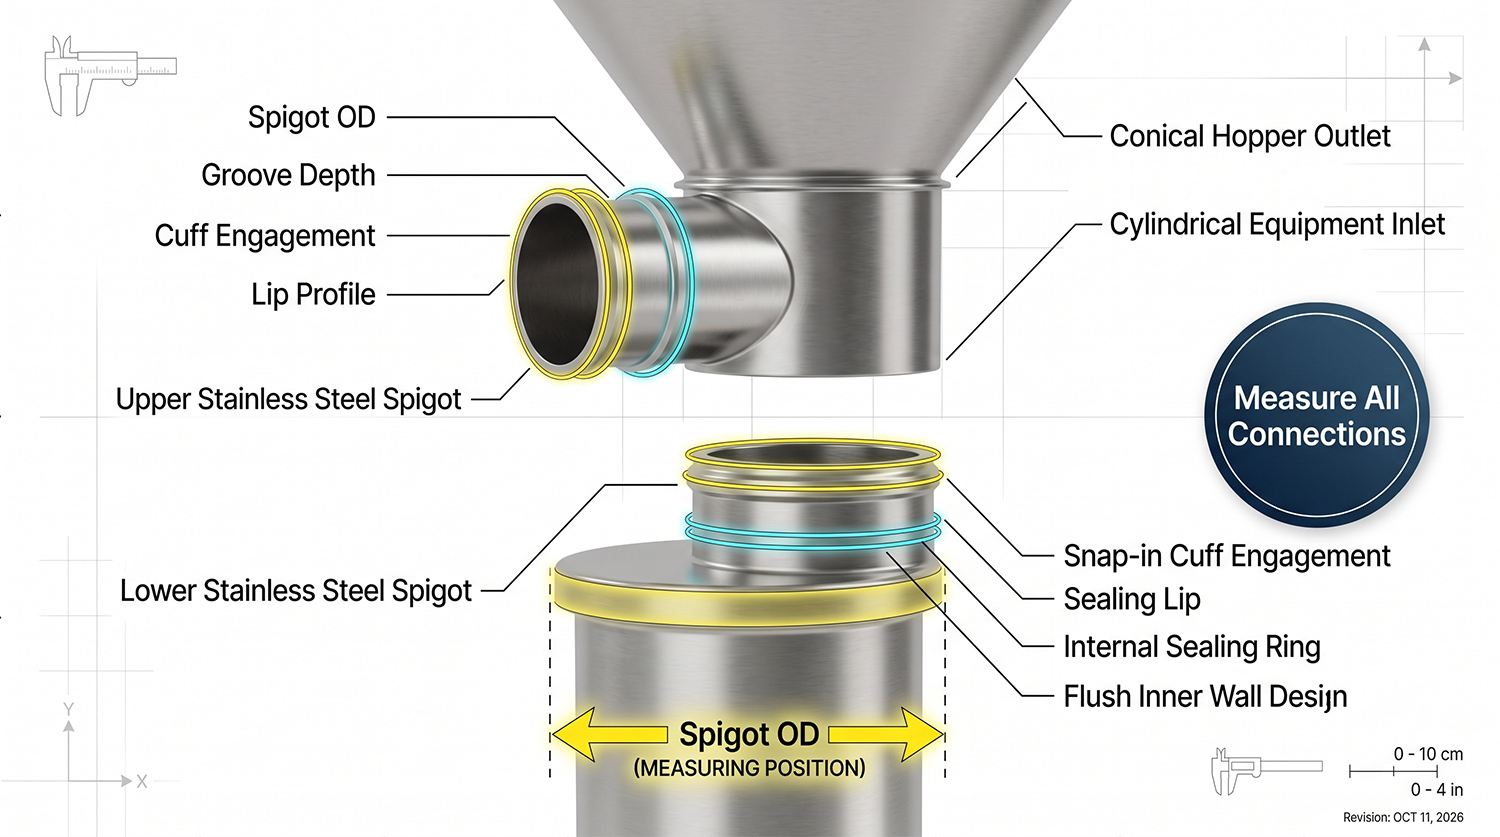 Figure 1: Measure all metal connection points directly on the equipment interface. Always verify the rigid spigot OD (Outside Diameter), groove retention depth, and cuff seating profile with calipers.
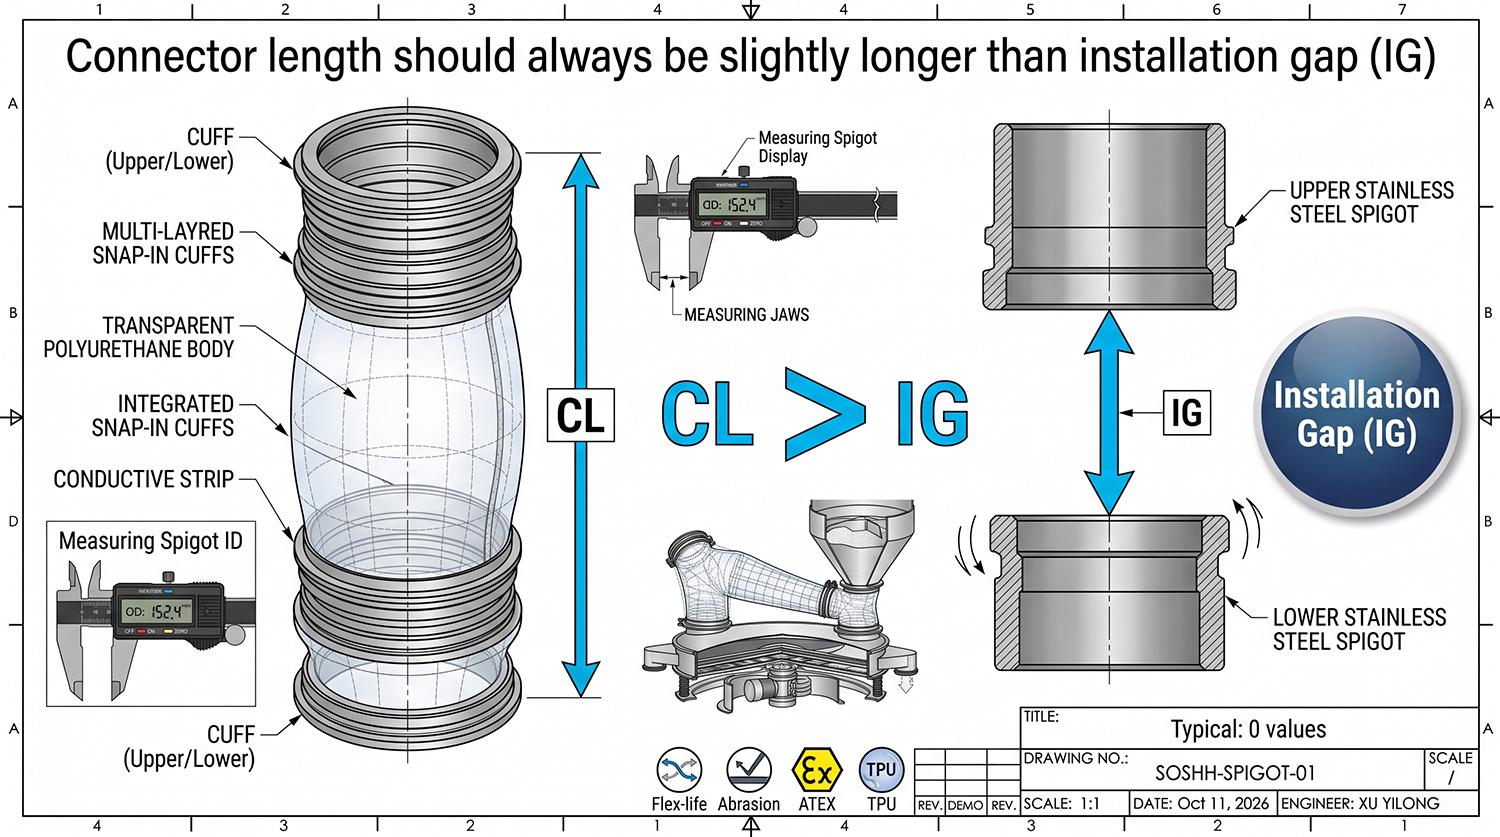 Figure 2: The sizing golden rule: The relaxed connector length (CL) must always be slightly longer than the static installation gap (IG) to accommodate vibration strokes without tensile cuff stress.
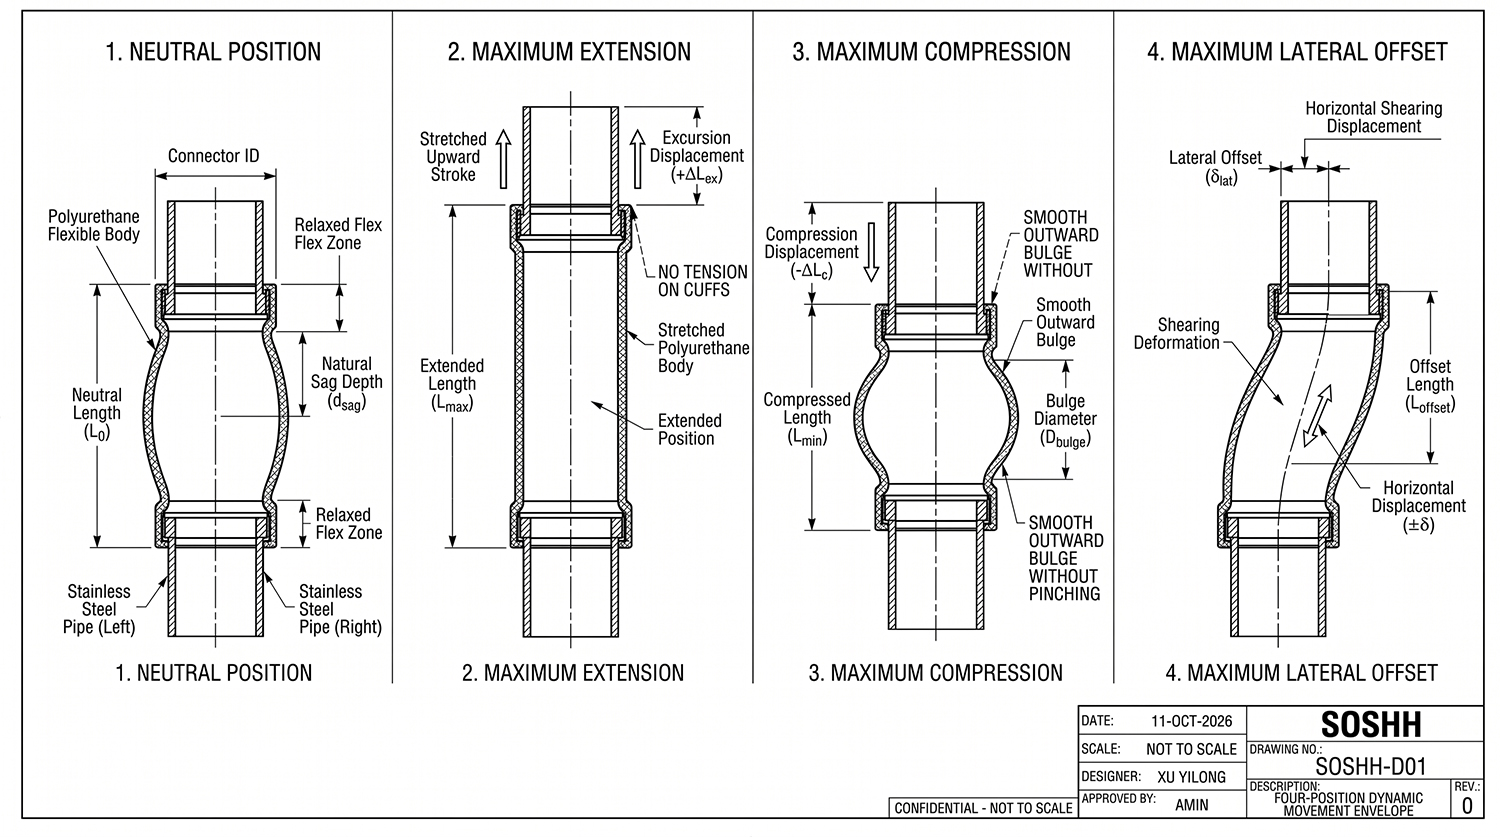 Figure 3: Four dynamic movement limits for vibrating equipment: Neutral (natural sag), Maximum Extension (no cuff tension), Maximum Compression (smooth outward bulge without material traps), and Maximum Lateral Offset (shearing absorption).