

How to Specify an Inflatable FIBC Bulk Bag Loading Seal for Powder Filling & Discharge
An inflatable FIBC loading seal uses a pneumatic bladder to apply radial sealing force around a bulk-bag neck. The required air pressure is construction-specific rather than universal; published designs range from sub-bar pneumatic operation to a product-specific 1–2 bar range. Correct sizing requires the actual neck diameter, liner thickness, sealing length, movement, temperature and filling-head pressure balance. The finished assembly should be tested under the intended filling conditions.
1. Why Conventional FIBC Connections Can Leak Dust
Traditional FIBC connections can work reliably when the bag neck, sealing surface and tightening procedure are well controlled. Problems arise when the connection depends on a flexible fabric-and-film interface being compressed uniformly by a manually installed mechanical device.
The main failure mechanisms are not all the same.
1.1 Bag-Spout Variability
FIBC necks are flexible textile structures rather than machined metal components. The actual interface can vary with fabric construction, liner installation, liner thickness, bag filling history, folding, sewing tolerances, neck ovality, temperature and manual positioning.
A connection designed around a nominal diameter can therefore see a larger or smaller effective sealing diameter during operation. Commercial bulk-bag loading equipment reflects this variability by allowing the sealing system to accommodate different bag-neck dimensions rather than treating one fixed diameter as universal. Published bulk-bag loader data show expandable neck ranges covering several hundred millimetres depending on the loader size.
1.2 Localized Clamp Pressure
A hose clamp or strap produces force through a relatively narrow contact region. The resulting pressure distribution depends on clamp geometry, clamp tension, sleeve stiffness, liner thickness, surface friction and local wrinkles. A nominally tight clamp can therefore have a locally high pressure point next to a low-pressure leakage path.
That does not mean every hose clamp connection leaks. It means clamp performance is sensitive to installation condition.
1.3 Liner Folding and Leakage Channels
A plastic liner can fold underneath the outer FIBC fabric. One small longitudinal fold can create a channel between the filling-head wall, liner, fabric and sealing element. Powder then preferentially follows the lowest-resistance path.
The important specification is therefore not merely “bag neck diameter = X mm.” It is “bag neck + liner + actual insertion geometry = controlled sealing interface.”
1.4 Operator Variability
Manual tightening introduces process variation. Two operators can produce different tightening torque, clamp position, liner overlap, insertion depth and re-tightening behavior. For low-cycle equipment this may be acceptable. For high-frequency FIBC filling, the connection procedure itself becomes a production variable.
1.5 Filling-Head Movement
The filling head may move relative to the bag during bag positioning, pre-inflation, filling, weighing, bag conditioning, discharge and release. Some bulk-bag filling systems deliberately combine inflatable sealing with adjustable bag support and tensioning because bag position and filling-head geometry affect stable filling.
A seal that works in a static bench test can behave differently when the bag neck is moving.
1.6 Venting Pressure Imbalance
A filling process moves powder into a flexible container while displaced air must leave. If the vent path is inadequate, pressure can rise inside the bag. Published bulk-bag filler designs commonly use a double-walled or double-casing fill head so displaced air and fines can be routed to a dust-extraction system rather than discharged into the room.
The inflatable seal therefore cannot be engineered independently from the fill-head air path.
1.7 Repetitive Mechanical Fatigue
Repeated bag installation and removal exposes the neck and sealing system to folding, compression, sliding, local abrasion, repeated inflation/deflation and temperature cycling. For a production line, connection life should be evaluated by cycle count rather than by a single successful installation.
2. How an Inflatable FIBC Seal Works
The functional architecture can be understood as four concentric zones:
Rigid Fill Spout → Inflatable Bladder → FIBC Neck / Liner → External Support Structure
The exact cross-section varies by manufacturer and application.
2.1 Rigid Core Spout
The rigid spout defines the process flow path and provides stable internal diameter, connection to the filling head, a dimensional reference for the flexible seal, and mechanical support during bag attachment. The rigid core may be stainless steel or another material appropriate to the process.
2.2 Pneumatic Bladder
Compressed air is introduced into the inflatable section. As the bladder expands, it applies radial pressure against the FIBC neck or liner. The objective is not maximum pressure. The objective is sufficient and reasonably uniform contact pressure over the designed sealing area.
2.3 FIBC Neck and Liner
The flexible bag neck is compressed between the inflatable sealing element and its mating surface. The seal must accommodate the actual neck OD/ID, fabric construction, liner thickness, liner folds, surface friction and axial tension.
2.4 External Structural Support
Some designs use a structural ring or reinforced external architecture to control geometry. The design should be evaluated for radial expansion, free-bore diameter, ring or support location, connection clearance, fatigue and cleanability.
3. Inflation Pressure: How to Specify It Correctly
“1.5 bar” is not a universal answer. Current published inflatable FIBC products show significantly different pneumatic requirements.
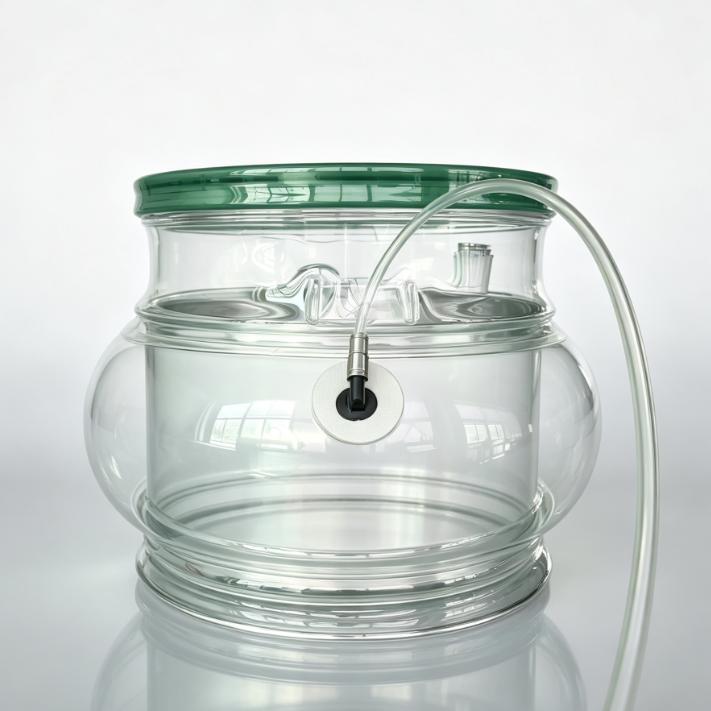
The current SOSHH product page lists a 1.0–2.0 bar operating air pressure and 6/8 mm push-in air fittings. These are product-specific specifications.
Another published bulk-bag loader uses an 8 mm pneumatic airline, recommends approximately 3–4 psi, and limits supply pressure to 6 psi with a pressure-relief arrangement.
The correct conclusion is: inflation pressure must be specified from the actual bladder design and verified by test.
3.1 Minimum Pressure
Too little pressure can produce incomplete circumferential contact, bag-neck slip, local powder leakage and sensitivity to neck variation. The minimum required pressure should be established by a retention and leakage test using the actual bag/liner combination.
3.2 Excessive Pressure
Too much pressure can increase liner compression, local film stress, bladder stress, deformation of the FIBC neck and release-force requirements. Do not infer liner contact pressure directly from supply pressure.
3.3 Pressure-Control Hardware
The pneumatic circuit should normally include a regulator, pressure gauge, isolation valve, controlled exhaust, pressure relief where required, and appropriate tubing and fittings. Published bulk-bag loader installation guidance recommends pressure regulation and a relief valve to avoid over-inflation, and requires the bag neck to be in position before inflation.
4. FIBC Neck and Liner Compatibility Matrix
FIBC spout dimensions are application-specific rather than one universal ISO dimension. ISO 21898:2024 establishes FIBC construction, design, testing and marking requirements for non-dangerous goods; it should not be treated as a catalogue of universal filling-neck diameters.
Commercial FIBC products commonly offer multiple filling and discharge spout dimensions, including examples around 350–500 mm and larger ranges depending on the bag design.
Commercial RFQ Starting Matrix
| PARAMETER | PRACTICAL RFQ STARTING POINT | ENGINEERING TREATMENT |
|---|---|---|
| Bag neck nominal diameter | 350 mm | Confirm actual supplied OD/ID |
| Bag neck nominal diameter | 400 mm | Confirm actual supplied OD/ID |
| Bag neck nominal diameter | 450 mm | Confirm actual supplied OD/ID |
| Bag neck nominal diameter | 500 mm | Confirm actual supplied OD/ID |
| Liner construction | Form-fit LDPE | Verify actual liner material and folds |
| Liner construction | Tubular PE / PE-based film | Verify film thickness and weld construction |
| Barrier liner | PE/EVOH multilayer | Verify surface and compressibility |
| Conductive liner | IEC-classified FIBC liner system | Confirm FIBC/liner classification and grounding method |
| Barrier foil construction | Aluminum-containing multilayer | Perform process-specific electrostatic and sealing assessment |
| Commercial liner thickness | 50–150 μm starting range | Confirm exact supplied thickness; not an ISO universal value |
| Sealing engagement | 150–250 mm as an engineering starting range | Verify actual contact length and retention |
| Surface friction | Project-specific μs / μk | Obtain test data for the actual liner/seal pair |
| Neck ovality | Measure actual maximum/minimum OD | Do not qualify only to nominal diameter |
| Neck insertion depth | Record actual installed dimension | Control mechanically in FAT/SAT |
| Bag-neck length | Supplier-specific | Confirm minimum available sealing length |
| Liner overlap | Supplier-specific | Record overlap and wrinkle condition |
| Temperature | Actual process range | Verify seal performance at operating temperature |
50–150 μm, 150–250 mm and 350–500 mm are starting engineering ranges or commercial reference examples, not international standards. The final drawing should use measured bag-neck dimensions.
5. FIBC Type C, Type D and Liner Electrostatics
FIBC electrostatic classification is a separate issue from the inflatable seal’s mechanical design.
IEC 61340-4-4:2018 classifies FIBC as Type A, B, C or D and also addresses inner-liner classification and safe use in hazardous explosive atmospheres.
Type C FIBC uses conductive construction and is designed to be connected to earth before filling/emptying and remain connected during those operations.
Type D FIBC uses static-protective construction and is designed to control electrostatic risk without an earth connection to the FIBC itself.
The connector RFQ should therefore not simply say “ATEX bag.” It should identify the FIBC type, liner classification, required grounding method, conductive components, hazardous-area assessment and powder charging characteristics.
Where a conductive liner is used with a Type C FIBC, its earth connection must be deliberate and mechanically robust; accidental contact with the FIBC fabric should not be treated as the grounding method.
6. Sealing Force vs. Bag-Neck Damage
A useful first-order force model is:
Fᵣ ≈ ΔP × Aₑff
Where Fᵣ is the effective radial sealing force, ΔP is the bladder pressure relative to the surrounding space, and Aₑff is the effective pressure area of the bladder.
This is a design relationship, not a finished-product rating formula. The actual contact pressure around the circumference also depends on bladder shape, material stiffness and local geometry.
6.1 If the Force Is Too Low
Possible results: dust escape, axial slip, leakage at liner folds, sensitivity to bag-neck variation.
6.2 If the Force Is Too High
Possible results: liner deformation, local film yielding, creasing, abrasion, excessive bladder strain, difficult release.
There is no defensible universal rule such as “below 0.5 bar leaks” or “above 2.5 bar tears PE.” Those values depend on the finished geometry and actual liner material.
6.3 Edge Geometry
The sealing interface should avoid abrupt pressure transitions. Recommended features include radiused support edges, smooth transition surfaces, no sharp metal edges under the liner, controlled insertion depth, enough engagement length and no local pinching at the end of the sealing zone.
6.4 Friction and Retention
An approximate axial retention model is:
Fₐₓ,retention ≈ μ × N
Where μ is the effective friction coefficient of the actual mating surfaces and N is the normal force.
Because μ changes materially between PE films, coated textiles and different seal materials, the friction coefficient should be measured or documented for the actual interface. Do not import a generic friction coefficient from a handbook and treat it as the installed FIBC value.
7. Filling vs. Discharge: Different Dynamic Requirements
The same inflatable seal may be used for both filling and discharge, but the process loads are not identical.
7.1 Filling
The filling process can include powder inflow, displaced air, entrained air, bag expansion and filling-head movement. Bulk-bag filling systems commonly use a filling head with air-volume balancing and dust extraction because air displaced by incoming powder must leave the bag in a controlled manner.
During high-rate filling, the bag neck can move, the bag body expands, the liner unfolds, powder can create transient local pressure changes, and displaced air carries fines toward the vent system. The seal must therefore be checked dynamically.
7.2 Discharge
During discharge, material exits through the connection, the bag neck may contract, air can enter or leave depending on the receiving equipment, and the flexible neck can become less stable as the bag empties. Bottom-discharge systems may therefore need different mechanical support from a top-filling head.
7.3 Inflation and Deflation Control
Inflation should achieve the required retention before filling begins. Deflation should be controlled so the bag can be released, the liner is not trapped, the operator is not exposed to sudden mechanical release, and the bladder returns to its intended rest position. A controlled exhaust valve can be useful where cycle time matters.
8. Integrated Dust Extraction and Pressure Balance
A bulk-bag filling station is an air-and-solids system.
A useful first-order displacement equation is:
Q(displaced) = (ṁ powder ÷ ρ bulk) + Q(entrained air)
Where Q(displaced) is the gas volume that must be accommodated by the vent path, ṁ powder is the powder mass flow rate, ρ bulk is the bulk density, and Q(entrained air) is the additional air entering the bag/fill system.
Bulk density is defined as mass divided by occupied bulk volume and includes the air voids within the bulk material. The formula gives a useful first-order volume term, but it does not eliminate the need to measure or estimate additional gas flow.
8.1 Why Extraction Must Be Sized as a System
If extraction capacity is inadequate, displaced air may pressurize the bag, fines may escape at the sealing interface, and the filling head may see back pressure.
If extraction is excessive, the system can draw additional air through intended or unintended leakage paths, thin liners may deform, filling behavior can change, and powder may become excessively aerated depending on the process.
Published industrial filling systems demonstrate that dust extraction is an integral part of the fill-head design rather than a separate afterthought. Some commercial systems specify dedicated dust-removal capacities in the hundreds of cubic metres per hour, but these values are equipment-specific and should not be copied as a universal setpoint.
8.2 What to Measure
For commissioning, record pressure at the fill head, pressure at the dust-collector takeoff, airflow, powder throughput, bag mass, filling time and seal leakage condition. Do not specify a universal “−50 to −150 Pa” target without system validation.
9. Changeover Economics and Labor Model
The economic advantage of an inflatable seal is easiest to quantify when a plant changes FIBCs frequently.
Annual Labor Cost = N bags × (T connection ÷ 60) × R labor
Where N bags is the number of bag changes per year, T connection is the connection time in minutes, and R labor is the loaded labor cost per hour.
9.1 Illustrative Example
Assume:
- 5,000 bags/year
- Conventional clamp connection = 3 min/bag
- Inflatable connection = 15 sec/bag
- One operator
- Loaded labor rate = $60/hour
Conventional clamp:
5,000 × 3 ÷ 60 = 250 hours/year 250 × $60 = $15,000/year
Inflatable connection (15 sec = 0.25 min):
5,000 × 0.25 ÷ 60 = 20.83 hours/year 20.83 × $60 ≈ $1,250/year
Illustrative labor difference:
250 − 20.83 = 229.17 hours/year 229.17 × $60 ≈ $13,750/year
These numbers are illustrative assumptions, not an industry benchmark. The plant should substitute actual observed connection time, actual labor rate, number of operators, cleaning time, inspection time, rework, dust-cleanup time and production downtime.
Link: Flange vs Clamp vs Snap-In TCO Engineering Guide → https://www.soshh.com/pages/flange-vs-clamp-vs-snap-in-tco
10. Troubleshooting and Failure Modes
| SYMPTOM | DIRECT MECHANISM | ROOT ENGINEERING CAUSE | FIELD DIAGNOSTIC STEP | CORRECTIVE ACTION |
|---|---|---|---|---|
| Dust escapes around bag neck | Incomplete circumferential seal | Neck OD variation, liner fold, insufficient or uneven bladder expansion | Inflate with the actual bag installed and inspect the full circumference | Confirm neck dimensions, liner condition, engagement length and pressure range |
| Bag neck slips during fill | Axial retention force is insufficient | Low normal force, low friction, dynamic bag movement | Apply the actual fill-head movement while monitoring neck position | Recheck pressure, sealing geometry, engagement and bag support |
| Liner wrinkles badly | Local compression creates folds or channels | Excessive local pressure or incorrect liner insertion | Inspect liner before and after inflation | Improve insertion procedure, edge radius and bladder geometry |
| Bladder is slow to deflate | Restricted exhaust flow or pneumatic dead volume | Small exhaust path, hose restriction, valve selection or contaminated fitting | Measure deflation time with and without the bag installed | Increase exhaust capacity, shorten tubing or revise valve arrangement |
| Powder accumulates above sealing ring | Product is reaching a ledge or stagnant region | Incorrect insertion depth, geometry mismatch or fabric/liner fold | Open and inspect after a representative filling cycle | Modify geometry, insertion depth or cleaning access |
| Seal works empty but leaks during filling | Dynamic pressure/movement changes the interface | Bag expansion, displacement air, head movement or liner migration | Test at production feed rate and extraction condition | Run dynamic FAT/SAT at actual fill rate and ventilation condition |
| Bladder ruptures prematurely | Local fatigue, abrasion or over-expansion | Excessive pressure, sharp geometry, repeated cycling or mechanical interference | Inspect fracture location and compare with expansion path | Review pressure limit, support geometry, clearance and cycle qualification |
11. Qualification Protocol: FAT, SAT and RFQ Specification Builder
A good inflatable FIBC seal should be accepted as a tested assembly, not simply as a component that fits the nominal diameter.
11.1 Ten Recommended Qualification Tests
These are recommended engineering qualification activities, not universal standards or mandatory acceptance values. The customer should define the required acceptance criteria.
Test 1 — Dimensional Fit. Verify spout OD, neck ID/OD, sealing length, insertion depth and free-bore diameter.
Test 2 — Static Seal Test. Install the actual FIBC neck and liner, inflate to the specified operating condition, and check for visible leakage, neck movement and liner migration.
Test 3 — Inflation/Deflation Cycling. Perform a defined number of production-equivalent cycles. A plant may specify a target such as 10,000 cycles where the expected lifecycle justifies that qualification, but the number should be treated as a project requirement rather than a universal industry standard.
Test 4 — Axial Retention Test. Apply the expected axial load from bag weight, filling-head movement, tensioning system and discharge operation. Record slip or movement.
Test 5 — Dynamic Filling Test. Run the actual powder or a validated process simulant. Measure leakage, bag-neck movement, filling stability and extraction behavior.
Test 6 — Pressure-Control Verification. Verify regulator accuracy, relief setting, operating range, pressure stability and controlled deflation.
Test 7 — Liner Compatibility. Repeat the test with the actual liner material and thickness. Do not qualify an LDPE liner and assume identical behavior with a multilayer barrier or conductive liner.
Test 8 — Cleaning / Washdown Test. Where applicable, verify chemical exposure, seal performance after cleaning, bladder condition and connection integrity.
Test 9 — Electrical / Electrostatic Assessment. Where combustible dust is involved, verify the complete applicable electrical-control strategy. For FIBC systems, use the relevant FIBC classification and liner requirements of IEC 61340-4-4:2018. Type C systems require grounding during filling/emptying, while Type D relies on its defined static-protective construction without grounding the FIBC itself. Do not substitute a single continuity number for the entire hazardous-area assessment.
Test 10 — Post-Cycle Inspection. Inspect bladder, liner contact area, external reinforcement, snap-in connection, pneumatic fitting, welds, seals and surface condition. Record any permanent deformation or damage.
12. RFQ Specification Builder
Send the following information when requesting an inflatable FIBC seal.
FIBC Geometry
| PARAMETER | RFQ INPUT |
|---|---|
| Spout Core OD | ____ mm |
| FIBC Neck ID | ____ mm |
| FIBC Neck OD | ____ mm |
| Bag Neck Flat Width, if supplied | ____ mm |
| Neck Length | ____ mm |
| Available Sealing Length | ____ mm |
| Insertion Depth | ____ mm |
| Neck Ovality | ____ mm maximum/minimum |
| FIBC Bag Type | Type A / B / C / D / other |
| Liner Type | LDPE / multilayer PE / EVOH / conductive / barrier / other |
| Liner Thickness | ____ μm |
| Liner Construction | Form-fit / tubular / gusseted / other |
Process Conditions
| PARAMETER | RFQ INPUT |
|---|---|
| Powder | __________ |
| Bulk Density | ____ kg/m³ |
| Particle Size | ____ |
| Flowability | __________ |
| Filling Rate | ____ kg/h |
| Target Bags per Hour | ____ |
| Filling Temperature | ____ °C |
| Cleaning Temperature | ____ °C |
| Cleaning Method | Dry / CIP / COP / other |
| Dust Extraction Pressure at Head | ____ Pa |
| Dust Extraction Flow | ____ m³/h |
| Filling Head Movement | ____ mm |
| Dynamic Stroke | ____ mm |
| Vibration | ____ mm / ____ Hz |
Pneumatic Requirements
| PARAMETER | RFQ INPUT |
|---|---|
| Available Air Pressure | ____ bar |
| Required Operating Pressure | ____ bar |
| Tubing OD | ____ mm |
| Fitting Standard | Push-in / NPT / BSP / other |
| Relief Requirement | Yes / No |
| Deflation Requirement | Manual / automatic |
| Cycle Time | ____ s |
Compliance Requirements
| PARAMETER | RFQ INPUT |
|---|---|
| Food Contact | Yes / No |
| FDA Documentation Required | Yes / No |
| EU Food-Contact Documentation | Yes / No |
| Hazardous Area | Yes / No |
| Zone | 20 / 21 / 22 / other |
| FIBC Electrostatic Type | C / D / other |
| Grounding Required | Yes / No |
| Metal Detector | Yes / No |
| Magnet Downstream | Yes / No |
| Copper/Zinc Restriction | Yes / No |
| Product Contamination Limit | __________ |
13. What to Put on the Engineering Drawing
A good drawing should show more than “Ø400 × 300 mm.” It should define:
- Rigid spout ID/OD
- Sealing surface
- Minimum/maximum bag-neck diameter
- Minimum engagement
- Neutral installed length
- Inflation inlet
- Pressure operating range
- Pressure relief requirement
- Deflation path
- Material
- Temperature range
- Cleaning condition
- Reinforcement arrangement
- Inspection points
The supplier should also state which dimensions are nominal, minimum, maximum, or qualification-controlled.
14. How to Handle Food, Pharmaceutical and High-Containment Applications
Food-contact and pharmaceutical applications require more than a generic statement such as “food grade.”
For the finished connector and FIBC interface, verify the exact polymer formulation, additives, liner material, sealing element, operating temperature, contact duration, cleaning agents and intended food or pharmaceutical use.
ISO 21898:2024 applies to FIBC construction and safety for non-dangerous goods, while hygienic or food-contact requirements can arise from separate regulatory and equipment-design frameworks. The inflatable connector and the FIBC liner should be evaluated as a combined product-contact interface.
15. When an Inflatable Seal Is the Right Architecture
An inflatable FIBC seal becomes particularly attractive when several of these conditions are present:
- Frequent bag changes
- Fine powder
- High dust-containment requirements
- Operator-dependent manual clamping
- Variable bag-neck diameter
- Rapid bag release
- Pharmaceutical or food hygiene requirements
- Integrated dust extraction
- High-throughput bulk-bag filling
- OEM equipment requiring repeatable connection geometry
Commercial bulk-bag filling systems already use inflatable seals together with bag tensioning, pressure balancing and dust extraction, demonstrating that the seal should be designed as part of the filling-head system rather than treated as an isolated flexible sleeve.
16. When a Conventional Clamp May Still Be Appropriate
An inflatable seal is not automatically the correct solution for every FIBC connection.
A conventional mechanical connection can still be reasonable where bag changes are infrequent, neck dimensions are tightly controlled, operator access is easy, dust-containment requirements are modest, no automated cycle is required, pneumatic utilities are unavailable, or the existing equipment is already qualified and stable.
The decision should be based on process requirement, connection frequency, risk, maintenance method and total lifecycle cost.
17. Final Engineering Decision Sequence
Specify the connection in this order:
- Measure the actual FIBC neck.
- Identify the liner material and thickness.
- Define the required sealing engagement.
- Define filling and discharge conditions.
- Define available pneumatic pressure.
- Establish the required inflation range from the actual seal design.
- Integrate dust extraction and pressure balance.
- Check FIBC electrostatic classification where applicable.
- Test retention, leakage and cycle performance.
- Compare lifecycle cost against the existing connection method.
This sequence prevents the most common purchasing error: selecting the connector from nominal bag diameter first and discovering the mechanical, liner or pressure problem after installation.
Frequently Asked Questions
What pressure should an inflatable FIBC seal operate at? There is no universal industry pressure. Current published designs range from sub-bar pneumatic operation to a product-specific 1–2 bar range. Specify the actual pressure envelope for the selected bladder construction and validate it with the installed bag neck.
Is 1.5 bar the standard pressure for bulk-bag inflatable seals? No. It can be a product-specific value, but published systems use different pressure ranges. One documented loader recommends approximately 3–4 psi and a maximum of 6 psi.
What FIBC neck diameter should I specify? Use the actual bag supplier’s measured neck dimensions rather than assuming a universal standard. Commercial bag and loader systems cover multiple diameter ranges, including examples around 350–500 mm and beyond.
Does ISO 21898 define the filling-spout diameter? No. ISO 21898:2024 covers FIBC materials, construction, design, testing and marking for non-dangerous goods; it should not be treated as a universal catalogue of neck diameters.
Can an inflatable seal be used with an FIBC liner? Yes, provided the seal is qualified with the actual liner. LDPE, multilayer and electrostatic-control liners can have different thickness, friction and deformation behavior.
What liner thickness should I use? Do not choose liner thickness from a universal standard value. A commercial RFQ may start around 50–150 μm for some liner constructions, but the exact bag supplier specification must be confirmed.
Can an inflatable seal replace a mechanical clamp? It can provide the sealing and retention function for a compatible design, but the complete system must still be evaluated for bag-neck geometry, pressure, movement and release.
How do I calculate the required dust-extraction airflow? Use the first-order balance: Q(displaced) = (ṁ powder ÷ ρ bulk) + Q(entrained air). Then account for the actual filling-head geometry, pre-inflation air, conveying air and dust-collection system. Do not use a universal exhaust airflow value.
Should the fill head run at a fixed negative pressure? Not as a universal rule. The required pressure balance depends on the filling-head architecture, powder, throughput and dust-collection system. Measure and validate the actual process.
Does Type C FIBC need grounding? Yes. IEC 61340-4-4 defines Type C FIBC as conductive constructions designed to be connected to earth during filling and emptying. Type D FIBC is a different construction and does not require the FIBC itself to be connected to earth in the same way.
Does an inflatable connector automatically make an FIBC system ATEX compliant? No. The connector is only one component of the electrostatic and hazardous-area assessment. FIBC classification, liner type, grounding, conductive parts, equipment category and site risk assessment must be considered together. IEC 61340-4-4 addresses FIBC electrostatic classification and testing; it is not by itself an ATEX certification statement.
How many inflation cycles should the seal survive? Use the expected plant lifecycle to define the qualification target. A project may specify 10,000 cycles or more, but cycle count should be treated as a project acceptance criterion rather than a universal standard.
What causes a bag neck to slip even when the bladder is inflated? Common causes include insufficient normal force, low friction, inadequate engagement length, liner folding, excessive dynamic movement and incorrect pressure settings.
What information should I send for a quotation? At minimum: bag-neck OD/ID, neck length, liner material and thickness, filling rate, bulk density, available air pressure, dust-extraction condition, operating temperature, connection dimensions and any food-contact, electrostatic or metal-control requirements.
Request an Inflatable FIBC Seal Engineering Review
Provide the bag neck OD, neck length, liner material/thickness, filling rate, bulk density, available air pressure, installed dimensions and dust-extraction condition. The engineering review can then determine the required sealing geometry, pneumatic configuration, connection dimensions and qualification plan.
Request an Inflatable FIBC Connector Review
Inflatable FIBC Bulk Bag Loading Seal